

Linija za profilisanjeLinia CZS
Zeman


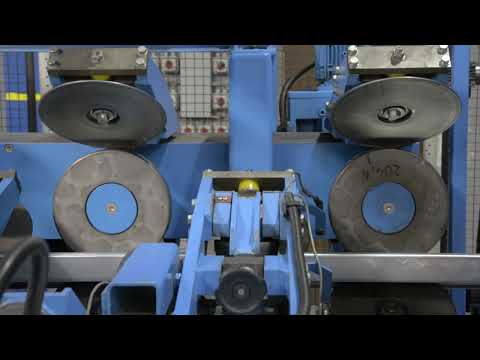


Podaci o mašini
- Naziv mašine:
- Linija za profilisanje
- Proizvođač:
- Linia CZS
- Model:
- Zeman
- Godina proizvodnje:
- 2010
- Stanje:
- skoro nov (polovno)
- Funkcionalnost:
- potpuno funkcionalan
Cijena i lokacija
- Lokacija:
- Mariusza Bojemskiego 9, 42-202 Częstochowa, Polska
Detalji ponude
- ID oglasa:
- A21299532
- Ažuriranje:
- posljednji put 22.07.2026
Opis
ZEMAN CZS LINE SPECIFICATIONS
ZEMAN's flagship product, the fully automated "PURLIN" line, is used to produce open, cold-formed sections such as C, Z, and SIGMA, in various widths and shapes, thanks to fully automatic adjustment of the profiling rollers. Coils up to 750 mm wide and 1.25 mm to 3 mm thick sheet metal in grade S-390 and lower can be used as raw material. The machine is designed to produce components up to 15 m long. The width of the specially hardened profiling rollers is infinitely adjustable, using only dedicated software. A fully integrated "flying punching" device creates all types of mounting holes, and the entire process is continuous, meaning the material does not stop for individual operations such as punching holes or cross-cutting. To maintain production efficiency, the line speed is dynamically optimized. The machine decelerates and accelerates automatically without operator intervention.
A coil uncoiler with a maximum working load of 15 tons is mounted on a mobile trolley, enabling precise centering of the material strip before feeding it into the straightener.
The straightener, along with a crescent straightening system, allows for straightening the material, ensuring the required sheet flatness and reducing the crescent on the feed belt.
2. Punching Section
This section contains 5 double, "flying" punching portals, which can be equipped with 20 small (up to 40 mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
A combination of these tools can also be used.
3. Pre-cutting Shear
A "flying" shear used to make preliminary holes for the cutting shear. This process is designed to maintain material continuity, resulting in a more precise profile shape, especially at its beginning and end. This is an adaptive guillotine that adjusts the width of the hole being cut to the width of the sheet metal strip.
4. Guide Carriage/SIGMA Modules
The guide carriage is used to center the sheet metal strip before entering the profiler. It is interchangeable
with the module for producing Sigma-shaped profiles. To produce S+ profiles,
the guide table should be removed and two Sigma modules inserted. These modules position
fully automatically and independently, left and right.
6. Rotary Cut-Off Guillotine.
The rotary cut-off guillotine with hook knives is used to finally cut the profile from the material strip
using the holes made by the pre-cutting guillotine. This is a "flying" guillotine,
so the sheet metal does not stop during the cutting process. Depending on the profile being produced, a properly oriented cutting cassette should be attached.
7. Receiving Table
Iedpfx Asymampedhjbb
The receiving table is used to automatically discharge the completed profiles from the roller conveyor. The elements are then manually arranged into a package. The design allows for easy bundling of the package. The table is designed to accept 15-meter profiles and allows for access by a forklift or overhead crane to collect the package of profiles.
Dobavljač
Registriran od: 2006
188 Oglasi online

Pošaljite upit
Telefon & Faks


 Švedska
OkumaLB 3000 EX II with Iemca KID 80


 Wilbertoord
DMGDMU 40 Evo Linear


 Root
OKUMALB 15


 Mađarska
DMG MORICMX 600 V




 Düsseldorf
DECKEL MAHOHSC 55 linear + system 3R


 Ulft
FicepTipo G25LG (S/N 36098)


 Mostar
MazakVTC-300C II


 Saint-Genix-les-Villages
DECKEL MAHODMU 160 P duoBLOCK


 Unterschleißheim
BRIDGEPORTVMC 610 XP


 Beograd
GaspariniSlitter

Machineseeker-pečat povjerenja
Što je pečat povjerenja?
Machineseeker certificira odabrane prodavače s povjerenjem Machineseeker. Prije odobrenja, iskusni Machineseeker zaposlenici provode standardiziranu i temeljitu provjeru.
Šta provjeravamo?

Provjera
obrtnice ili izvatka iz trgovinskog registra
Provjera
poštanske adrese prodavača
Validacija
bankovne veze
Potvrda
telefonske
dostupnosti glavnog broja
Ekonomska informacija
ne smije sadržavati negativne karakteristike
Žalbe kupaca
mogu dovesti do oduzimanja oznakeŠta to znači za vas kao kupca?
Zahvaljujući Machineseeker pečatu povjerenja, kao kupac možete prepoznati pouzdane prodavače bez vlastite provjere, koji s velikom vjerovatnoćom vode pošten i ispravan posao.
Naravno, tokom procesa kupovine ipak mogu nastati nesuglasice. Machineseeker nije odgovoran za pravne prekršaje aktivnih kupaca ili prodavača na Machineseeker.